
On a self-stacking belt, every tier rests on the stack plates of the tier below. The angle of those plates is small, easy to overlook on a flat table, and decides how the tiers meet.
We check the stack plate angle on a self-stacking belt with an angle gauge against the approved drawing: on the formed plates during production, on the trial section before mass production, and again before shipment. Then we stack sections of belt to check that the upper and lower tiers engage as the drawing specifies.
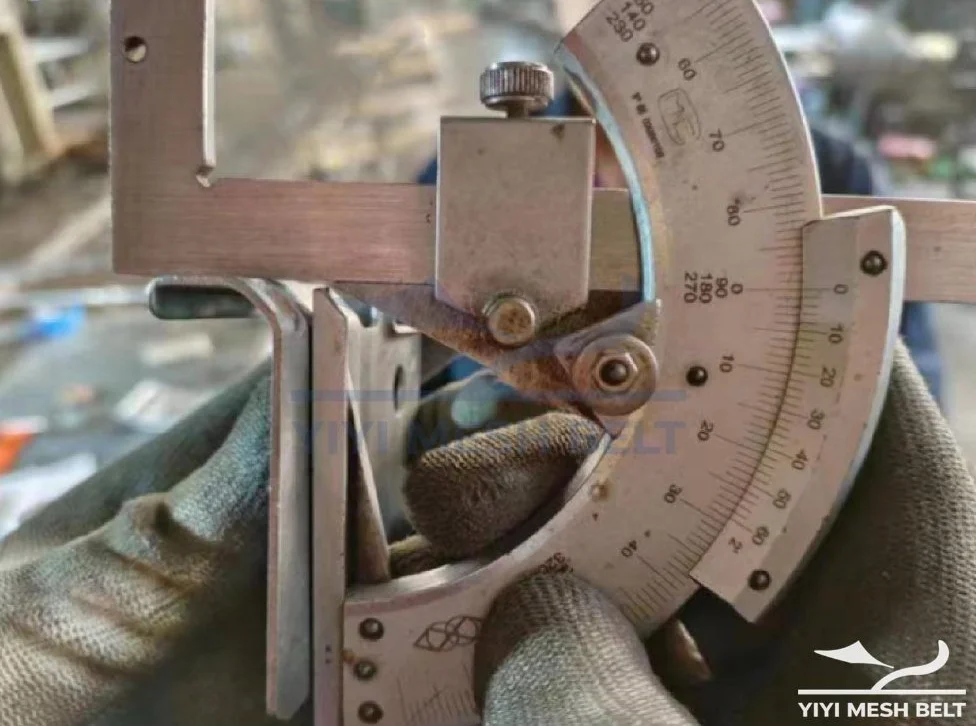
I am Sunny Ye, Global Sales Director at YIYI Mesh Belt (Ningjin Yiyi Mesh Belt Co., Ltd.). In our factory in Ningjin, the angle gauge on the stack plates is one of the in-process checks on every self-stacking belt. Here is what we measure, when, and why it matters for your spiral.
Contents
- What is the stack plate angle?
- Why does a small angle matter?
- How do we check the angle?
- How do we check that the tiers engage?
- What can you ask to see?
- When this is not the right choice
- FAQ
At a Glance
| Item | Details |
|---|---|
| Product | Self-Stacking Belt, stainless steel SUS304 / SUS316 |
| Part checked | Stack plate (side guard), 1.5 mm thick, 60 to 150 mm high |
| Reference | The plate geometry on the approved drawing |
| Tool | Angle gauge |
| When | Formed plates in production, trial section before mass production, final inspection |
| Follow-up check | Layer stacking and engagement of adjacent tiers |
What is the stack plate angle?
The stack plate is the side guard of a self-stacking belt. It is not a flat strip.
A stack plate is formed with bends that guide the tier above onto the tier below. The stack plate angle is the angle of those formed sections, set on the approved drawing for your equipment. Together with the guard height and the rod position, it fixes where the next tier lands.
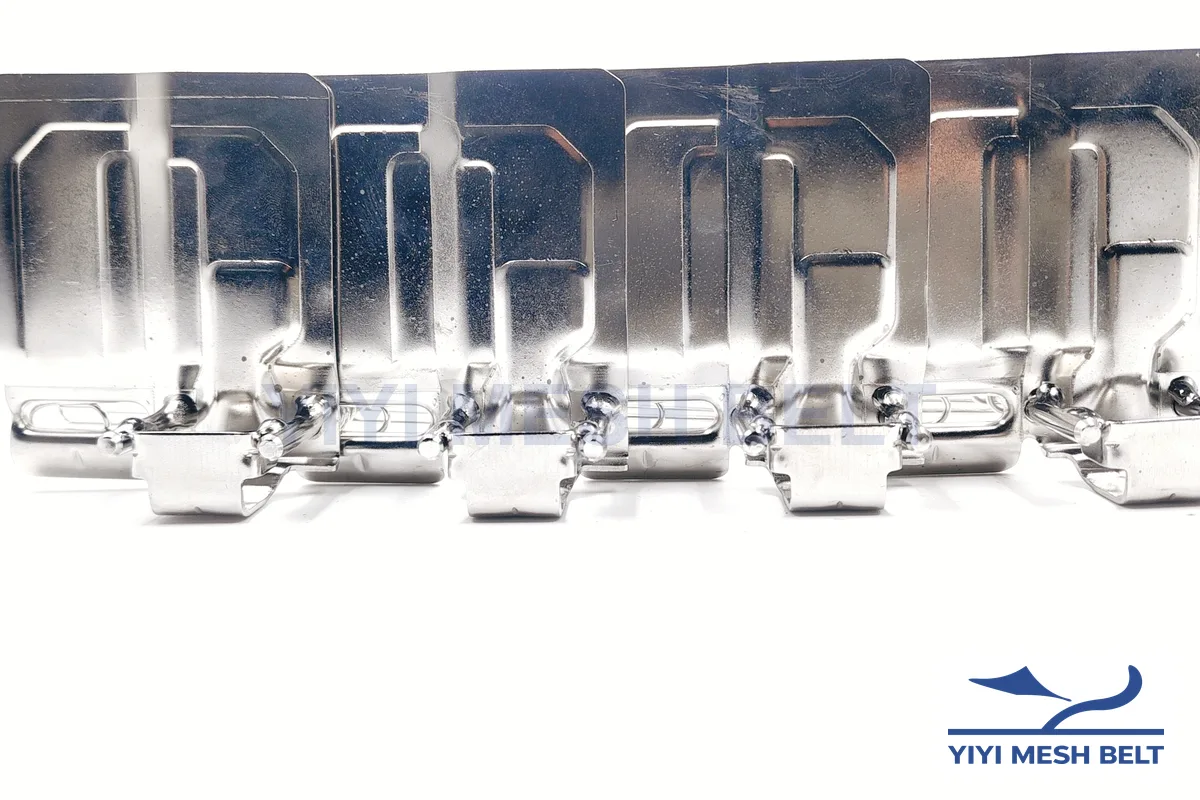
The geometry is project specific. On one recent order, for example, the drawing set the small foot at the bottom of each stack plate to a 45° bend. Another belt may use a different guard height and a different shape. That is why we check against your drawing, not against a general value.
| Parameter | Standard (mm) | Heavy duty (mm) | Inch (in), rounded |
|---|---|---|---|
| Side guard (stack plate) height | 60 / 80 / 90 / 100 / 120 | 80 / 100 / 150 | 2.36 / 3.15 / 3.54 / 3.94 / 4.72 / 5.91 |
| Side guard thickness | 1.5 | 1.5 | 0.06 |
| Stack plate angle | To approved drawing | To approved drawing | — |
| Rod-to-stack-plate gap | 1–2 | To approved drawing | 0.04–0.08 |
Why does a small angle matter?
One plate on a table tells you very little.
The plate angle decides how the upper tier lands on the lower one. A small angle error does not show on a flat table. It shows when ten or twenty tiers sit on top of each other in the freezer. That is why we check the angle during production, not only at the end.
A self-stacking belt carries its own weight. There are no rails holding each tier in place, as there are on a drum-driven spiral. So the stack plates do the work that rails do elsewhere, and their geometry has to agree with the equipment on every tier.
How do we check the angle?
We check the angle at three points, so an error is found while it is still one plate and not a whole belt.
We measure the stack plate angle with an angle gauge against the approved geometry: first on formed plates during production, then on the assembled trial section with its other dimensions, and finally in the inspection before packing. Trial pieces are checked against the approved geometry before production continues.
| Stage | What we check | Against |
|---|---|---|
| Plate forming | Stack plate angle and plate geometry on formed plates | Approved drawing |
| Trial section | Plate angle together with pitch, rod, wire, guard height and width | Approved drawing; first-article inspection |
| Layer engagement | Upper and lower tiers stacked to see how they meet | Approved equipment and belt design |
| Mass production | Formed components, assembly and weld condition | Approved trial section |
| Final inspection | Geometry, gap, welding and dimensions before packing | Approved drawing |
Every self-stacking belt order is also tested on a drum before shipment. The photos of each step are in our Self-Stacking Belt Production and Quality Control document (stack plate angle inspection is on page 10).
How do we check that the tiers engage?
The angle is a number. Engagement is the result you actually need.
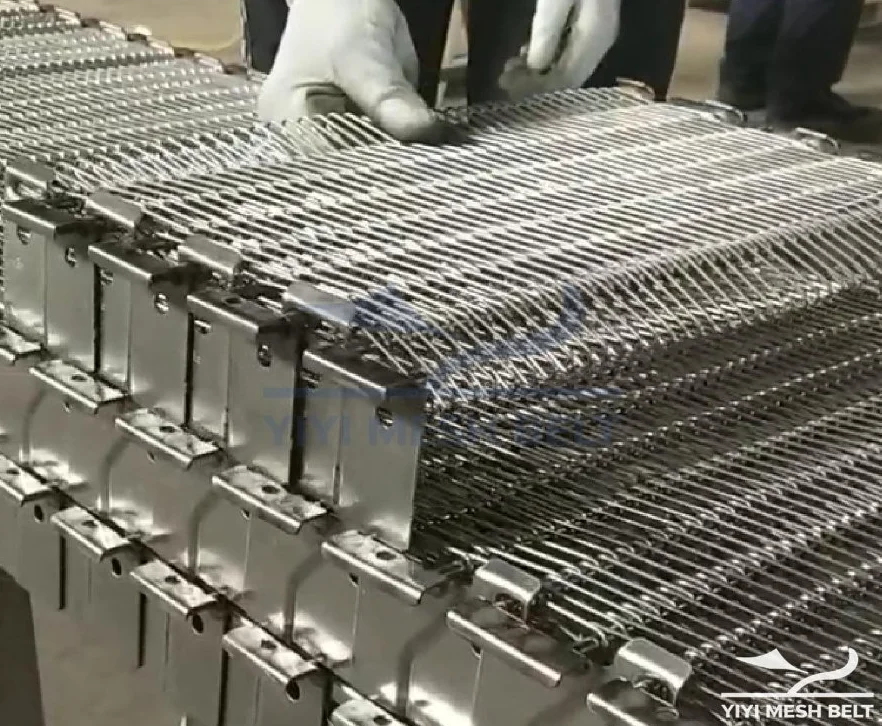
After the angle check, we stack sections of the belt on top of each other and check how the upper tier seats on the lower one. We do this on the trial section before mass production. Where the order asks for it, we check the stacking and engagement before, during and after welding.
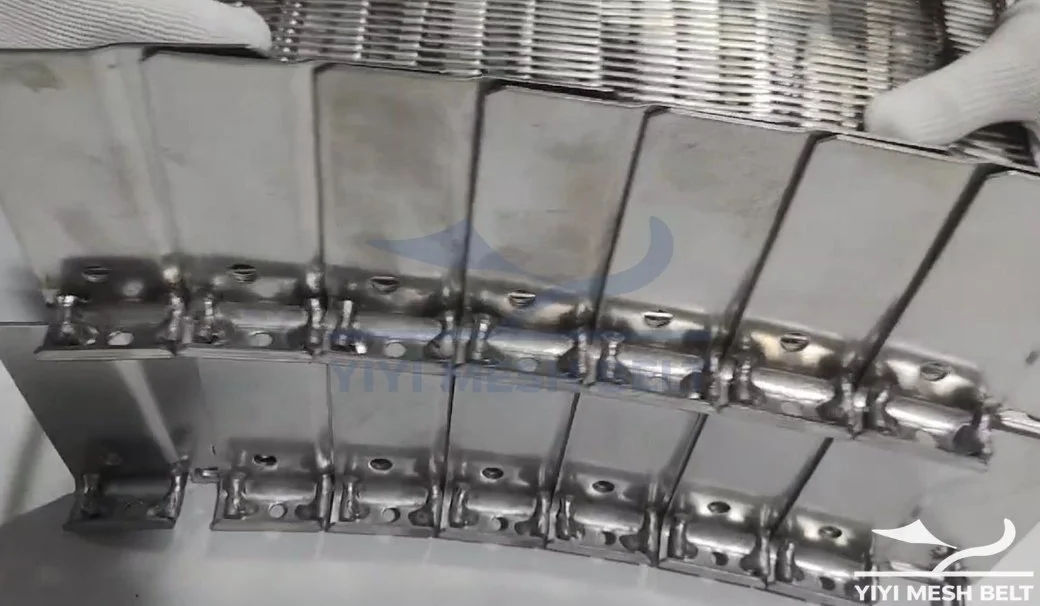
Welding is part of this because heat can move a plate. On a belt with tall 120 mm guards for a project in Australia (Oceania), the production order asked us to check the stacking and engagement of the upper and lower tiers before, during and after welding, and to keep the welding current low so the stack plate was not burned through.
What can you ask to see?
You do not have to take the check on trust.
Before you approve the trial section, ask for photos of the angle check and of the stacked tiers, together with the trial-section dimensions. We keep the inspection photos and your confirmations with the approved drawing, so the same geometry is used on every reorder.
| Item | What it shows you |
|---|---|
| Angle check photos | The stack plate angle measured on the formed plates |
| Stacked tiers photos | How the upper tier seats on the lower one |
| Trial-section dimensions | Pitch, rod, wire, guard height and width against the drawing |
| Edge close-ups | Rod ends, slots and the gap below the top of the stack plate |
If you are building to an old belt, you may also want to read how to confirm rotation direction and stack plates on a self-stacking belt.
When This Is Not the Right Choice
This check applies to self-stacking belts. A drum-driven Spiral Freezer Belt runs on rails and has no stack plates. And if you only have a worn belt, its plates may be bent from service, so they show the damage, not the original angle. In that case we confirm the plate geometry from your equipment drawing or from an unworn section before we approve anything.
From Our Engineering Experience
Buyers usually ask me about wire grade and width first. The plate angle comes up less often, yet it is the check I would least like to skip. A width error shows on the first metre. An angle error shows when the belt is already stacked in your freezer. My advice is simple: ask for the photo of the angle gauge on the trial section, and ask for the photo of two stacked tiers.
Evidence From Our Work
| Item | Details |
|---|---|
| Situation | A 760 mm SUS304 self-stacking belt, 20 m, with tall 120 mm stack plates, made with reference to the customer's sample |
| What we checked | A 0.12 m same-width sample was approved before material was prepared; stacking and engagement of upper and lower tiers checked before, during and after welding; low welding current at the stack plates |
| Why it matters | Taller plates carry the tier above over a greater height, so their geometry has to hold through welding |
| Buyer lesson | For tall guards, ask for the engagement check after welding, not only before |
| Item | Details |
|---|---|
| Situation | A 420 mm SUS304 self-stacking belt with 90 mm stack plates, collapsible on one side, made to the customer's sample |
| What we checked | The drawing set the small foot at the bottom of each stack plate to a 45° bend, a 1–2 mm gap below the top of the plate and a 5.5 mm long slot for the 5 mm rods |
| Result | 2 m test order in 2025, followed by a 100 m order in 2026 to the same data |
| Buyer lesson | Get the plate geometry on the drawing once, and every reorder follows it |
FAQ
What is the stack plate angle on a self-stacking belt?
It is the angle of the formed sections of the stack plate (side guard) that guide the tier above onto the tier below. It is set on the approved drawing for your equipment.
How do you measure the stack plate angle?
With an angle gauge, against the approved geometry: on formed plates during production, on the trial section before mass production, and in the inspection before packing.
Why is the angle checked before mass production?
A small angle error does not show on a flat table. It shows when many tiers are stacked in the freezer, so we find it on the trial pieces, before the full belt is built.
Do you check that the tiers engage?
Yes. We stack sections of the belt and check how the upper tier seats on the lower one on the trial section. Where the order asks for it, we also check before, during and after welding.
Can I see the angle check before I approve the belt?
Yes. Ask for photos of the angle check and of the stacked tiers with the trial-section dimensions. We keep them with the approved drawing for reorders.
Conclusion
The stack plate angle is small, project specific and easy to miss. We check it with an angle gauge on formed plates, on the trial section and before packing, then prove it by stacking the tiers.
Next step: Send us your drawing or photos of your stack plates for a production review. You can also reach me at info@yiyimeshbelt.com or on WhatsApp at +86 134 5177 3742. Product details: Self-Stacking Belt. Related reading: how a self-stacking belt is made, from wire to the stack check and why we keep a 1–2 mm gap between rod and stack plate.
Technical Reviewer: Sunny Ye, Global Sales Director, YIYI Mesh Belt (Ningjin Yiyi Mesh Belt Co., Ltd.) · Last updated: 2026-10-27
© 2026 Ningjin Yiyi Mesh Belt Co., Ltd. All rights reserved. Photos, drawings and data on this page belong to YIYI Mesh Belt and may not be copied or reused without written permission.

